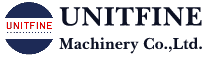
Choosing between a gyratory screen and a linear vibrating screen is not simply a question of which machine has the higher advertised capacity. The correct choice depends on the separation target, the percentage of near-size particles, material flow behavior, required product purity, available floor space, number of fractions, and how consistently the feed can be distributed across the screen.
This guide compares gyratory and linear screening from an engineering perspective. It explains how their motions affect material distribution, residence time, conveying, screen utilization, product handling, maintenance, and real production performance. The goal is to help plant engineers and purchasing teams define the right test conditions before selecting a bulk screener.
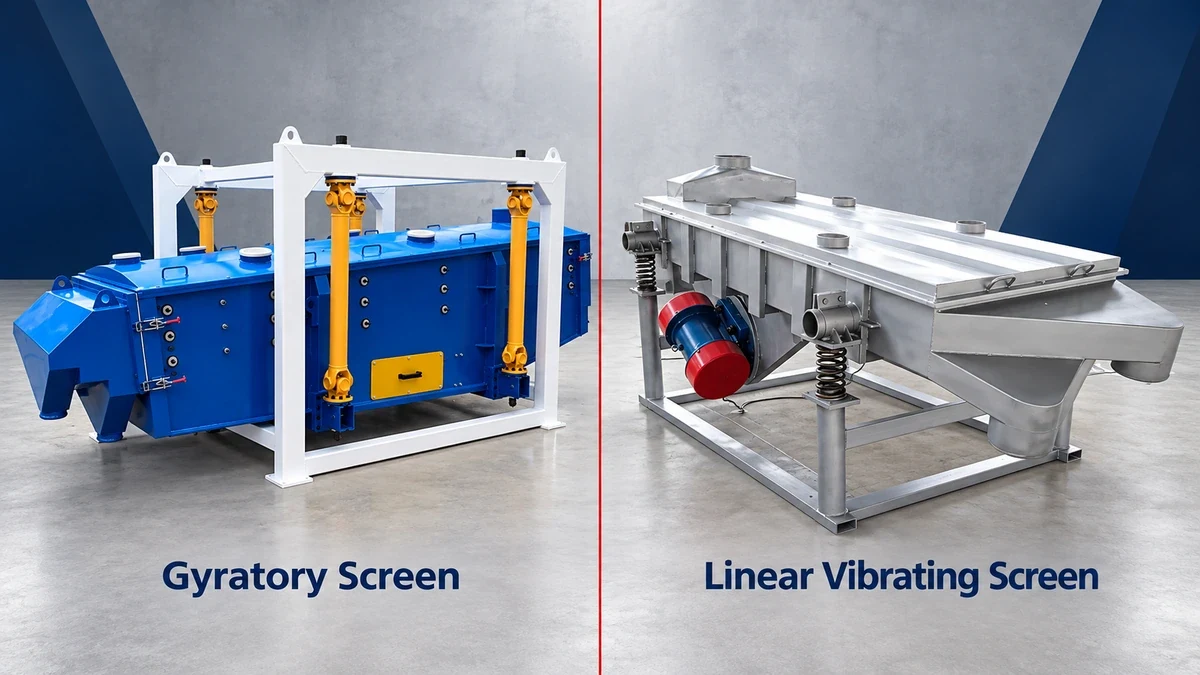
How the Two Screening Motions Work
Gyratory Screening Motion
A gyratory screener uses predominantly horizontal motion to spread and stratify material across a rectangular screen deck. The exact motion depends on the machine design. On the UNITFINE UF Gyratory Screener, the material path begins with a circular motion near the feed end, changes through an elliptical path, and approaches a straight-line motion near the discharge end. This progression helps distribute the feed, expose fine and near-size particles to the apertures, and convey oversize material toward the outlet.
Because vertical acceleration is limited compared with many vibrating screens, the material tends to remain in contact with the screen surface. That can support gentle handling and a longer screening opportunity, especially when the deck area, stroke, speed, feed loading, and mesh-cleaning system are matched to the product.
Linear Vibrating Motion
A linear vibrating screen commonly uses two synchronized counter-rotating vibratory motors. Their forces combine to create a directional motion that lifts and advances material along the screen. The UNITFINE UZSF Series Linear Vibrating Screen is designed for grading, separation, and dedusting of dry powders and granules through this linear transport action.
Linear motion is effective when the process needs positive forward movement, steady discharge, and robust handling of a continuous feed. Its performance still depends on feed distribution, deck angle, vibration settings, bed depth, screen length, aperture, and material characteristics. A narrow feed stream can underuse the available width, so the inlet and upstream feeder deserve as much attention as the screener itself.
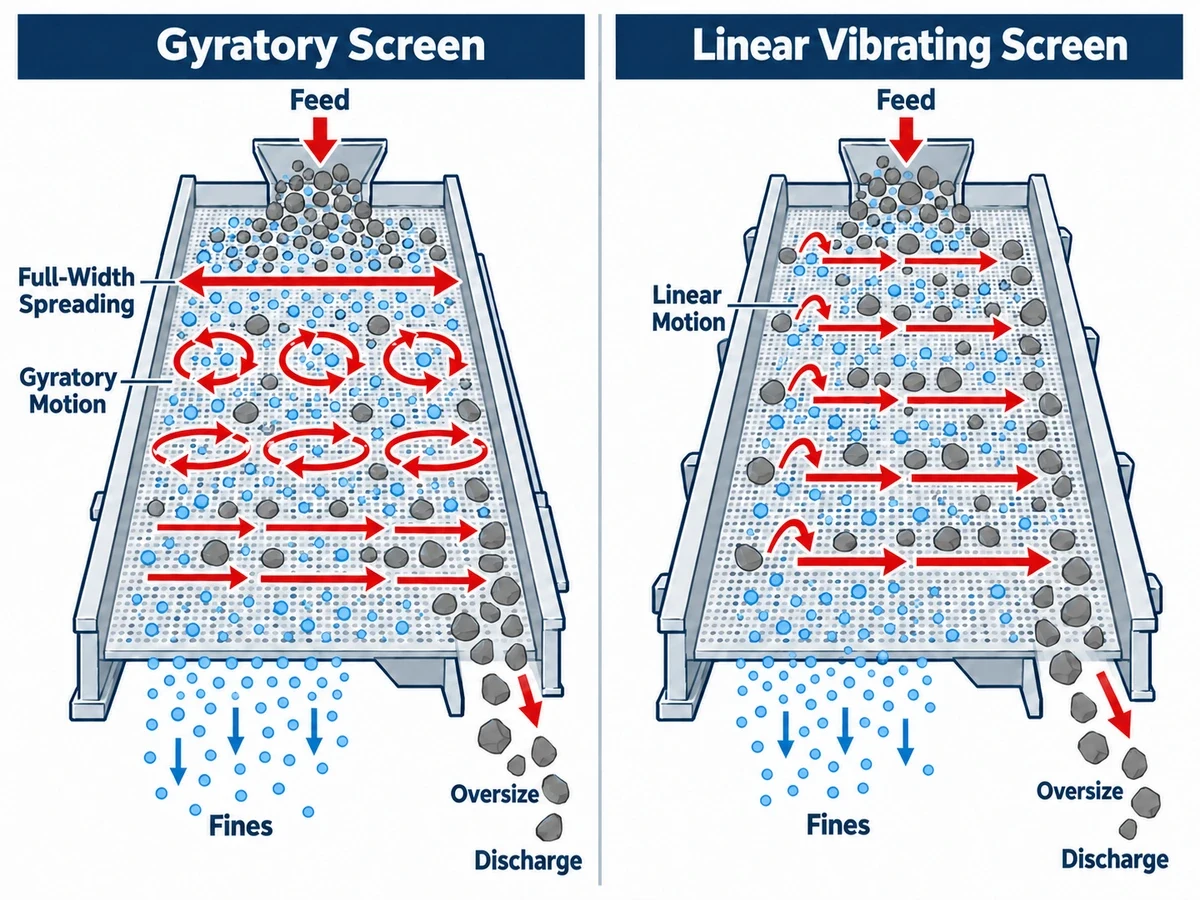
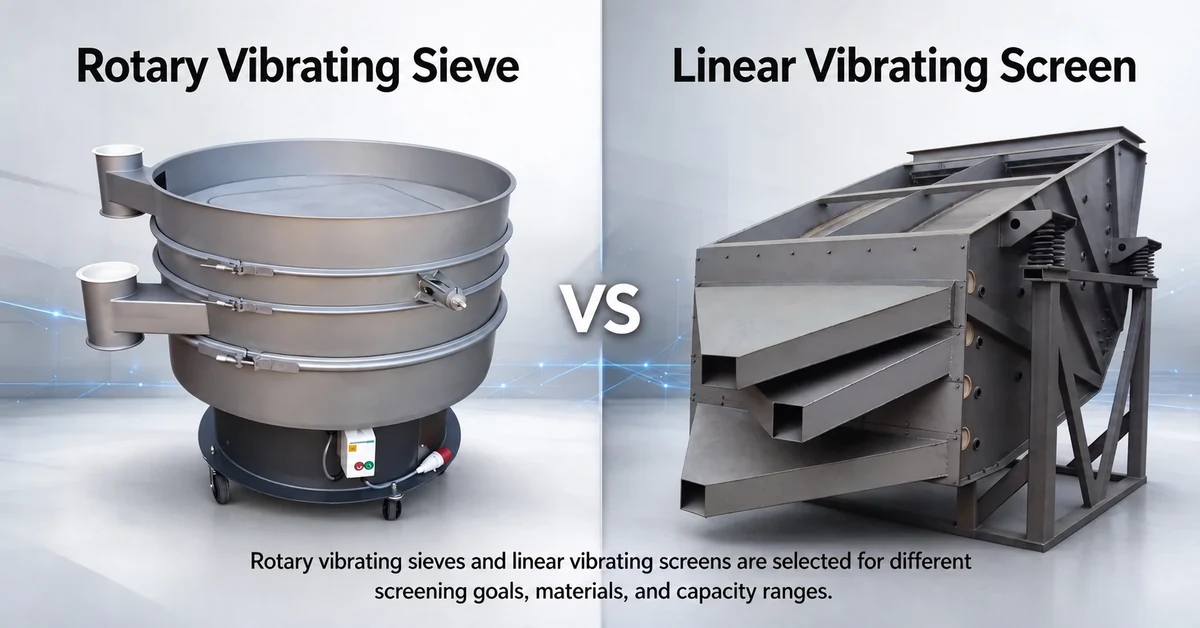
Gyratory Screen vs. Linear Vibrating Screen: Comparison Table
| Selection Factor | Gyratory Screen | Linear Vibrating Screen | What to Verify |
|---|---|---|---|
| Primary motion | Predominantly horizontal gyratory motion; the path may change along the deck | Directional vibration that lifts and advances material | Actual motion pattern, stroke, frequency, and adjustability |
| Typical strength | Often used for precise classification, broad material distribution, and longer screening opportunity when correctly configured | Often used for strong conveying, robust scalping or grading, and practical high-feed handling when correctly configured | Required product purity and accepted product loss |
| Near-size particles | Often favorable where near-size material needs more chances to find an aperture | Can perform well, but transport speed and bed depth must be controlled | Feed particle-size distribution around the cut point |
| Feed spreading | Gyratory action can spread a single feed stream across the deck | May need a full-width inlet or distributor for uniform loading | Usable screen width and loading profile during a test |
| Product handling | May support gentle handling because the referenced UF design emphasizes near-horizontal motion | Uses more active lifting and conveying; suitability depends on fragility, feed drop, loading, and settings | Fines generation, breakage, coating damage, and temperature |
| Capacity and footprint | A large rectangular area may support fine classification at the required quality, but the machine may be long | Often considered for high feed rates and a straightforward equipment arrangement, subject to cut-quality testing | Capacity at the required cut quality, not empty-machine rating |
| Multi-deck separation | Well suited to multiple product fractions when sufficient deck area and residence time are provided | Available in multi-deck arrangements for grading several fractions | Yield and contamination in every outlet stream |
| Typical maintenance focus | Suspension, drive, seals, screen tension, cleaning balls, and long-deck access | Motors, springs, deck fasteners, mesh tension, seals, and vibration transmission | Access time, screen-change method, spare parts, and isolation |
The table is a screening shortlist, not a guaranteed performance ranking. A properly configured linear screen can outperform a poorly sized gyratory unit, and the reverse is equally true. Always compare proposals at the same feed material, moisture, capacity, cut point, acceptable contamination, and operating schedule.
Seven Factors That Should Drive the Decision
1. Separation Accuracy and the Cut Point
Start by defining what “good separation” means. Is the task simple safety scalping, removal of occasional oversize contamination, or a tight product classification where misplaced near-size particles have a direct cost? Gyratory screening is often preferred for precision classification because material can spread across a large area and remain close to the mesh for a longer opportunity to pass.
A linear screen can be an excellent choice for scalping and general grading. For a demanding cut, however, its feed rate, bed depth, deck angle, screen length, and vibration settings must prevent near-size particles from reaching the discharge before they have enough presentation opportunities.
2. Real Capacity at the Required Product Quality
Throughput should never be evaluated alone. A screener may pass more tonnes per hour by carrying a deeper bed, but the extra loading can reduce contact with the mesh and increase misplaced material. The meaningful comparison is the stable feed rate achieved while meeting the required purity and recovery targets.
Ask each supplier to report feed rate, oversize and undersize mass balance, screen area, aperture, moisture, test duration, and the particle-size distribution of every outlet. This makes capacity claims comparable and prevents a fast but inaccurate test from appearing superior.
3. Feed Distribution and Screen-Area Utilization
A rectangular screen produces value only when its width and length are used effectively. Gyratory motion near the inlet can help distribute material across the deck. A linear unit may require a spreader, feed box, or wider inlet when material arrives as a concentrated stream.
During a test, observe the deck rather than only the discharge. Look for unused areas, localized overloading, uneven wear, material surfing above the bed, and excessive accumulation. A well-designed inlet can improve both screen life and separation without increasing machine size.
4. Material Flowability, Moisture, and Agglomeration
Free-flowing granules behave very differently from fine, cohesive, electrostatic, oily, or slightly damp powders. Gyratory and linear screens can both suffer blinding when the material is incompatible with the selected aperture and cleaning method. The correct question is not simply “Which motion is better?” but “Which motion, mesh, cleaning system, and feed condition keep this material screening consistently?”
If fine-powder agglomeration or mesh blockage is the dominant problem, an ultrasonic vibrating sieve or another deblinding approach may be worth evaluating for a suitable fine, dry powder. Compatibility with the material, mesh, required cut, cleaning method, and operating environment must still be confirmed by application testing.
5. Product Fragility and Fines Generation
Granules, coated particles, seeds, food pieces, and other fragile products can lose value if aggressive movement creates breakage or dust. Gyratory motion is generally gentle because it emphasizes horizontal movement. Linear vibration produces more active lifting and conveying, although careful operating settings can still handle many products successfully.
For fragile material, test the feed and all outlet streams. Measure or visually compare breakage, fines, coating damage, temperature rise, and any change in bulk density. A short visual demonstration without before-and-after samples is not enough.
6. Floor Space, Headroom, and Process Connections
Gyratory screeners may require a longer rectangular footprint, plus access for deck removal and inspection. Linear screens can also be long, but their simpler directional flow may fit naturally between an upstream feeder and downstream conveyor. Neither machine should be selected from the equipment outline alone.
Include the inlet transition, feeder, oversize and undersize chutes, dust connections, isolation devices, maintenance clearance, supporting structure, and access platform in the layout. A compact machine can still create a tall or difficult installation if a separate feed distributor is needed above it.
7. Cleaning, Changeover, and Maintenance
Plants that change products frequently may value screen access and cleanability more than maximum nominal capacity. Compare the number of decks, screen-tensioning method, gasket design, dead zones, internal corners, mesh-cleaning devices, tool requirements, and safe access to both sides of the machine.
Also consider how vibration is isolated from surrounding equipment. Linear screens rely on vibratory motors and springs, while gyratory units use their own drive and suspension arrangement. The foundation and support structure must suit the selected machine and operating load.
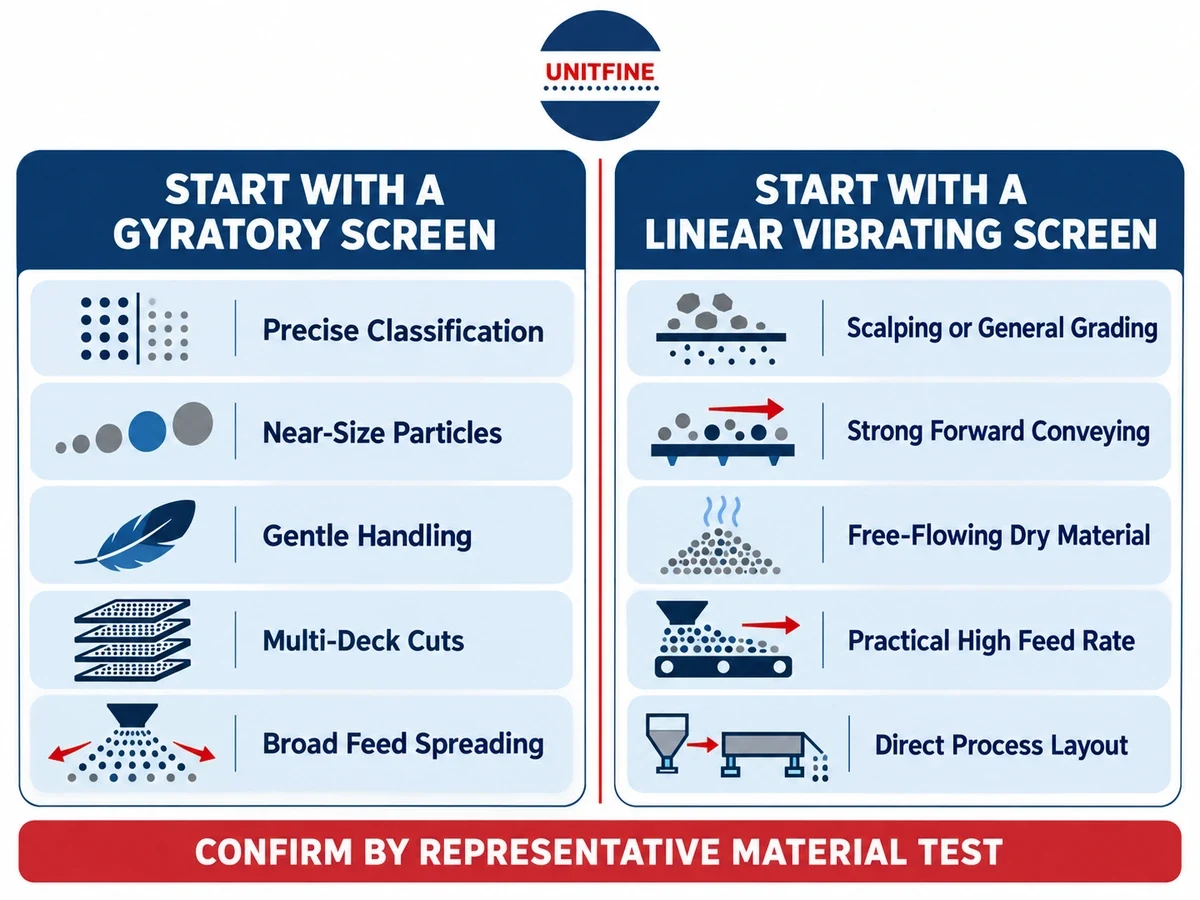
When a Gyratory Screen Is Usually the Better Starting Point
- The process requires a clean, precise cut rather than only rough scalping.
- A significant part of the feed is close to the aperture size.
- Gentle handling and low product breakage are important.
- Multi-deck classification must produce several controlled fractions.
- Uniform distribution across a wide rectangular deck is valuable.
- Longer screening opportunity is acceptable within the available footprint.
- The material is dry enough and suitable for the proposed mesh-cleaning system.
A gyratory screener is not automatically the right answer for every fine cut. Sticky material, severe agglomeration, very limited floor space, or an unsuitable feed system can still reduce performance. Confirm the exact motion, deck length, cleaning method, and access arrangement offered by the supplier.
When a Linear Vibrating Screen Is Usually the Better Starting Point
- The main duty is safety screening, scalping, dedusting, or general grading.
- Strong forward conveying and stable discharge are priorities.
- The material is free-flowing, dry, and not excessively sticky.
- The process benefits from direct conveying and a practical continuous-feed arrangement.
- The process layout favors a direct feed-to-discharge path.
- A suitable feeder or full-width inlet can distribute the material evenly.
- The required cut quality is demonstrated at the target production rate.
A linear screen should not be rejected simply because the application includes fine material. Screen length, aperture, loading, vibration settings, and feed distribution can materially change its performance. The decision should be based on a controlled test, not a generic rule.
A Practical Material-Test Protocol
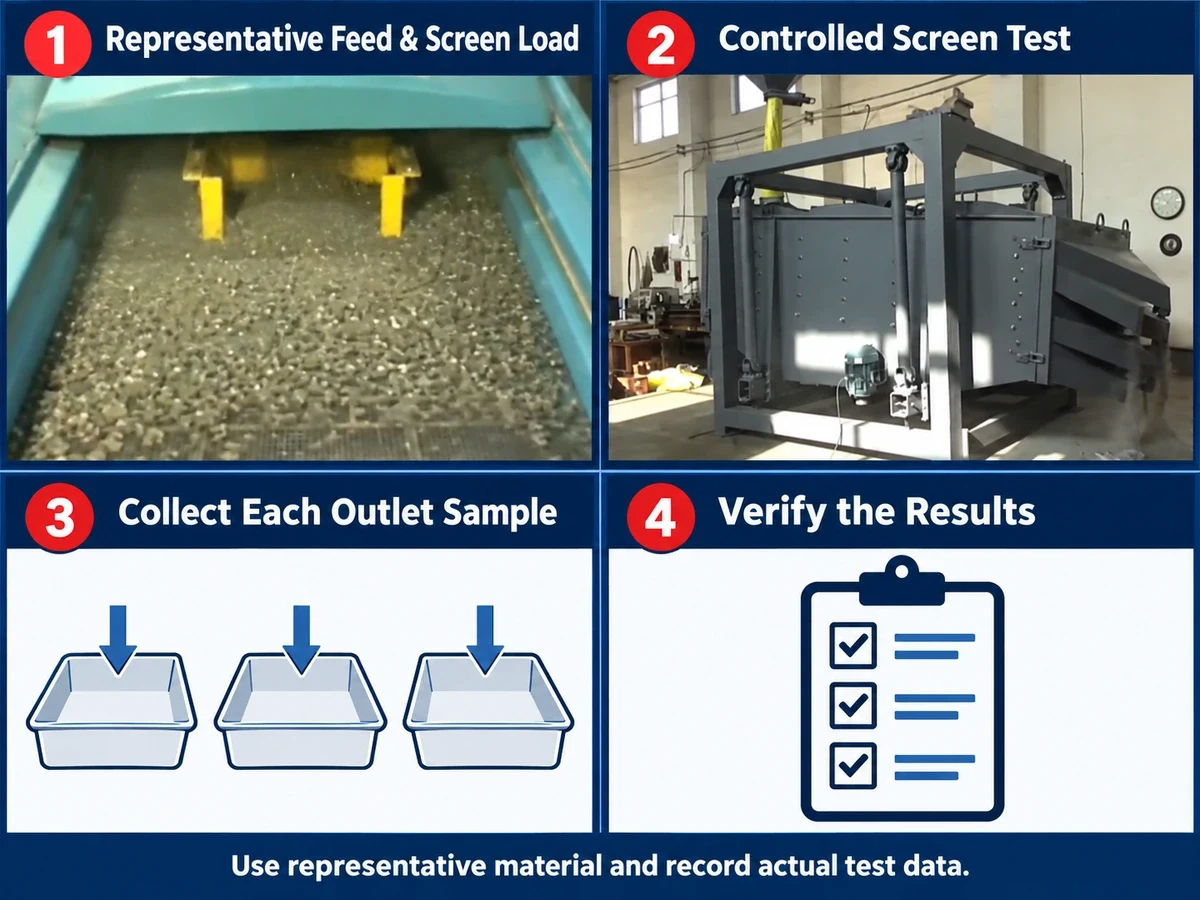
Before the test, agree on the target feed rate, cut point, sampling locations, test duration, calculation method, permitted mass-balance difference, and acceptance limits for misplaced material, recovery, purity, product damage, and screen condition. The limits must be defined for the tested material and proposed machine configuration rather than copied from a different application.
| Test Item | Information to Record | Why It Matters |
|---|---|---|
| Representative feed | Material name, lot, particle-size distribution, bulk density, moisture, temperature, and flow behavior | Prevents a dry or unusually easy sample from producing misleading results |
| Screen configuration | Machine model, deck dimensions, number of decks, aperture, wire type, deck angle, motion settings, and cleaning device | Makes the test repeatable and links performance to an actual configuration |
| Operating condition | Feed rate, feed distribution, test duration, bed depth, motor settings, and steady-state period | Distinguishes stable production from a short demonstration |
| Mass balance | Feed mass and mass from each outlet | Reveals yield, loss, and unexpected retention inside the machine |
| Separation result | Particle-size analysis of each fraction, misplaced material, recovery, and purity | Shows whether the required cut is achieved, not merely whether material passes through |
| Product and mesh condition | Breakage, fines, temperature, blinding, screen damage, dust leakage, and residue | Identifies quality, cleaning, and reliability risks before purchase |
Run long enough to reach a stable operating condition. If the process includes several products, test the most difficult material and the most demanding cut—not only the easiest item. Where product quality is critical, agree on the sampling method and acceptance criteria before the test begins.
Common Selection Mistakes
Comparing Nameplate Capacity Instead of Saleable Output
The highest feed rate is not useful if valuable product is lost to the wrong outlet. Compare saleable output, recovery, purity, and stability at the same production target.
Ignoring the Percentage of Near-Size Material
Two products with the same nominal particle range may screen very differently. A large near-size fraction demands more presentation opportunities and can expose differences in deck length, bed depth, and motion.
Testing Without the Real Feed Arrangement
A laboratory test with hand-spread material may not represent a narrow chute feeding one point in production. Reproduce the expected feed rate and distribution as closely as possible.
Choosing Mesh Size Without Studying the Whole Separation
Aperture is only one variable. Wire diameter, open area, deck tension, material shape, deck angle, vibration, and cleaning method all affect the result. Specify the required product fractions and let the final mesh selection follow testing.
How UNITFINE Can Help You Compare the Options
UNITFINE supplies both gyratory and linear screening solutions, so the selection can begin with the process rather than a single machine type. Review the complete fine screening equipment range, then provide a representative sample and clear acceptance criteria for the required separation.
For a useful recommendation, send the material name, particle-size distribution, bulk density, moisture, feed rate, required cut sizes, number of fractions, acceptable misplaced material, operating hours, product-contact material, available space, and cleaning requirements. Photos or drawings of the upstream and downstream equipment help identify inlet, outlet, and maintenance constraints.
For food, pharmaceutical, chemical, or combustible-dust duties, also state the required hygienic standard, cleaning procedure, material certificates, hazardous-area classification, dust characteristics, and applicable local safety requirements. These items require project-specific engineering review and are not established by the general comparison in this article.
Need a Screen Selection Review?
Send UNITFINE your material data, target capacity, cut sizes, product-quality requirement, and layout. Our team can review the application data, compare a UF Gyratory Screener with a UZSF Linear Vibrating Screen, and discuss whether a representative material test is available and appropriate for your project.
Frequently Asked Questions
What is the main difference between a gyratory screen and a linear vibrating screen?
A gyratory screen uses predominantly horizontal motion to spread and stratify material across the deck, while a linear vibrating screen uses directional vibration to lift and advance material. Gyratory screening is often selected for precise, gentle classification; linear screening is often selected for strong conveying, scalping, and practical high-feed grading.
Which screen gives a more accurate separation?
A gyratory screen often has an advantage for precise cuts and feeds containing many near-size particles because it can provide broad distribution and a longer screening opportunity. Accuracy still depends on aperture, deck area, loading, material condition, and machine settings, so the result must be confirmed for the tested feed and proposed configuration.
Which screen has the higher capacity?
There is no universal winner. A linear vibrating screen can handle high feed rates with strong forward transport, while a large gyratory deck can deliver substantial capacity at demanding cut quality. Compare both machines at the same purity, recovery, moisture, and operating conditions.
Is a gyratory screen better for fragile products?
It is often a good starting point because its motion is predominantly horizontal and generally gentle. However, product damage also depends on feed drop, deck loading, residence time, screen contact, discharge design, and downstream handling. Test before-and-after samples to confirm.
Can a linear vibrating screen make several product fractions?
Yes. Linear vibrating screens can be configured with multiple decks to separate several size fractions. The number of decks, cut sizes, feed distribution, screen area, and acceptable cross-contamination should be confirmed with the supplier and validated during testing.
What information does UNITFINE need to recommend a screener?
Provide the material, particle-size distribution, bulk density, moisture, normal and peak feed rate, required cut sizes, number of fractions, acceptable product loss, operating hours, contact material, cleaning method, available space, voltage, and upstream and downstream equipment.