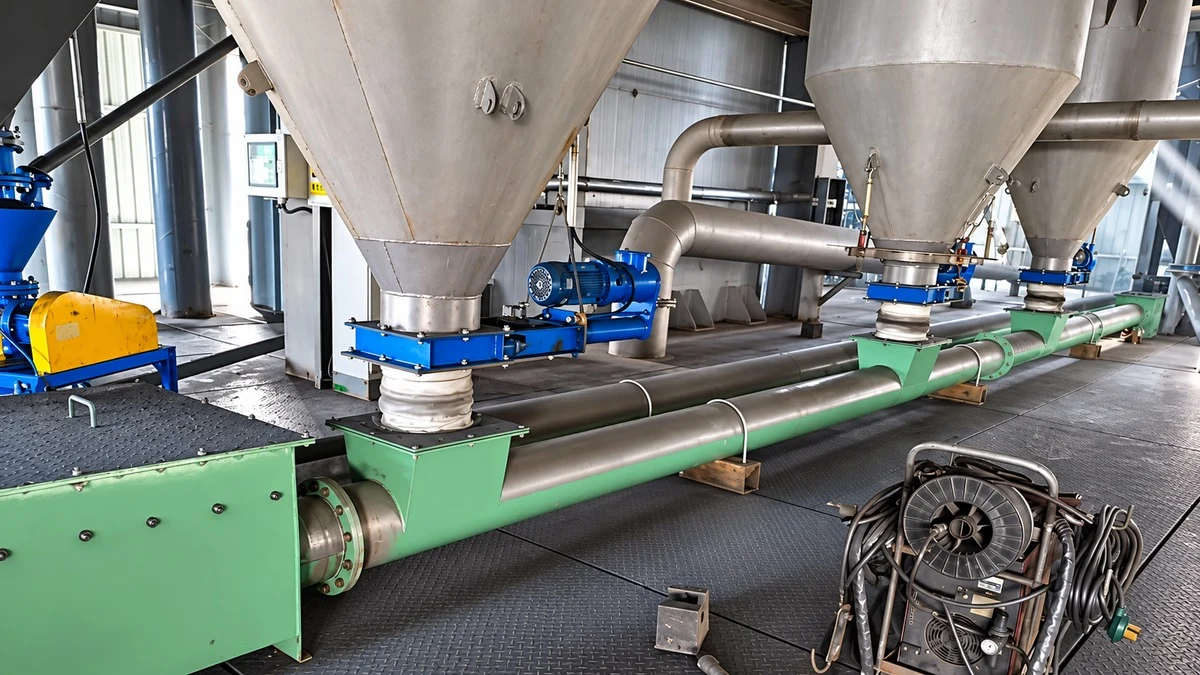
Tubular chain conveyor maintenance is not only about repairing a machine after it stops. For production plants that handle powders, granules, pellets, flakes, seeds, coffee beans, pet food, chemicals, or food ingredients, a maintenance plan helps protect conveying capacity, reduce unexpected downtime, and extend the service life of the chain, discs, tube sections, drive unit, bearings, seals, and inlet or outlet components.
A tubular chain conveyor works inside an enclosed pipe route, so many problems begin quietly: a slightly loose chain, worn discs, material build-up at an outlet, a noisy bearing, or a misaligned tension section. If these signs are ignored, they can become chain jamming, unstable conveying, product leakage, motor overload, or long production interruption. This guide explains practical maintenance best practices for tubular chain conveyor systems and gives plant teams a clear inspection routine.
Why Tubular Chain Conveyor Maintenance Matters
A tubular drag chain conveyor is often selected because it provides enclosed conveying, flexible routing, gentle material transfer, and low dust leakage. These advantages are strongest when the system is kept clean, correctly tensioned, and mechanically stable.
Maintenance becomes especially important in continuous production lines where the conveyor connects storage silos, mixers, screening machines, packing equipment, or downstream processing systems. One conveyor stop can interrupt several machines at the same time. For this reason, conveyor maintenance should be treated as production protection, not only equipment service.
Main Components That Need Regular Inspection
Before building a maintenance schedule, the operator should understand which parts are most likely to influence reliability. The exact structure depends on the conveyor model, route, material, and plant layout, but the following components are usually important.
| Component | What to Check | Why It Matters |
|---|---|---|
| Chain or cable assembly | Tension, elongation, abnormal wear, broken links, smooth movement | The chain or cable is the main moving part. Poor tension or damage can cause unstable conveying, jamming, or drive overload. |
| Conveying discs / flights | Wear, cracking, deformation, missing discs, material build-up | Disc condition affects conveying efficiency and material movement inside the tube. |
| Drive unit | Motor temperature, gearbox noise, vibration, coupling condition, lubrication | The drive unit supplies motion to the full conveying loop. Early signs of overload should not be ignored. |
| Inlets and outlets | Blockage, dust leakage, product build-up, valve operation, discharge flow | Most feeding and discharge problems begin around inlet and outlet points. |
| Tube sections and bends | Wear marks, dents, connection tightness, internal accumulation, alignment | Tube condition influences chain movement, material flow, and dust-tight performance. |
| Bearings and seals | Noise, heat, leakage, dust entry, grease condition | Bearing and seal failure can quickly become a downtime issue. |
Recommended Maintenance Schedule
The best schedule depends on running hours, material abrasiveness, moisture, cleaning frequency, and the value of uninterrupted production. The following plan is a practical starting point for many bulk material handling plants.
| Frequency | Maintenance Task | Operator Notes |
|---|---|---|
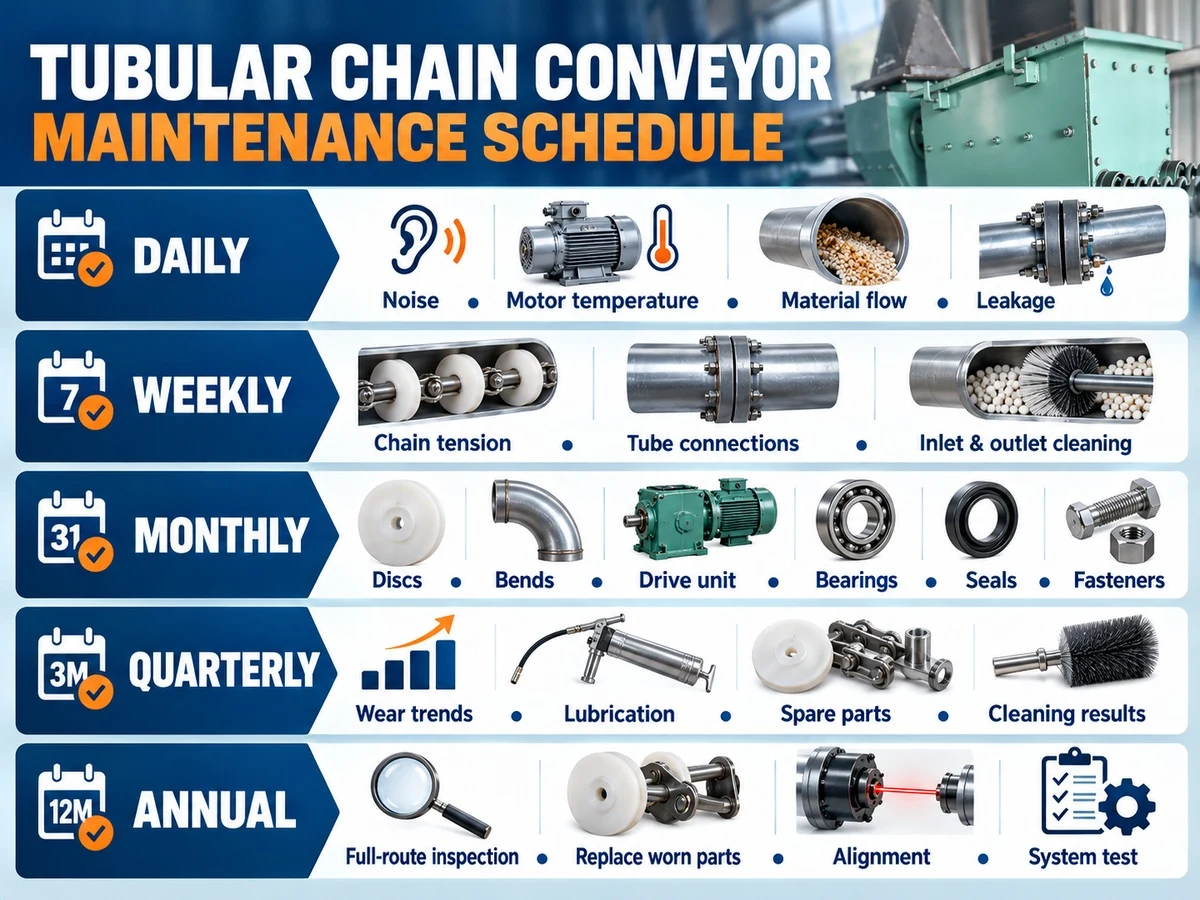
| Daily / each shift | Listen for abnormal noise, check motor temperature, watch inlet and outlet flow, inspect visible leakage. | Record unusual sound, vibration, current increase, or feeding instability immediately. |
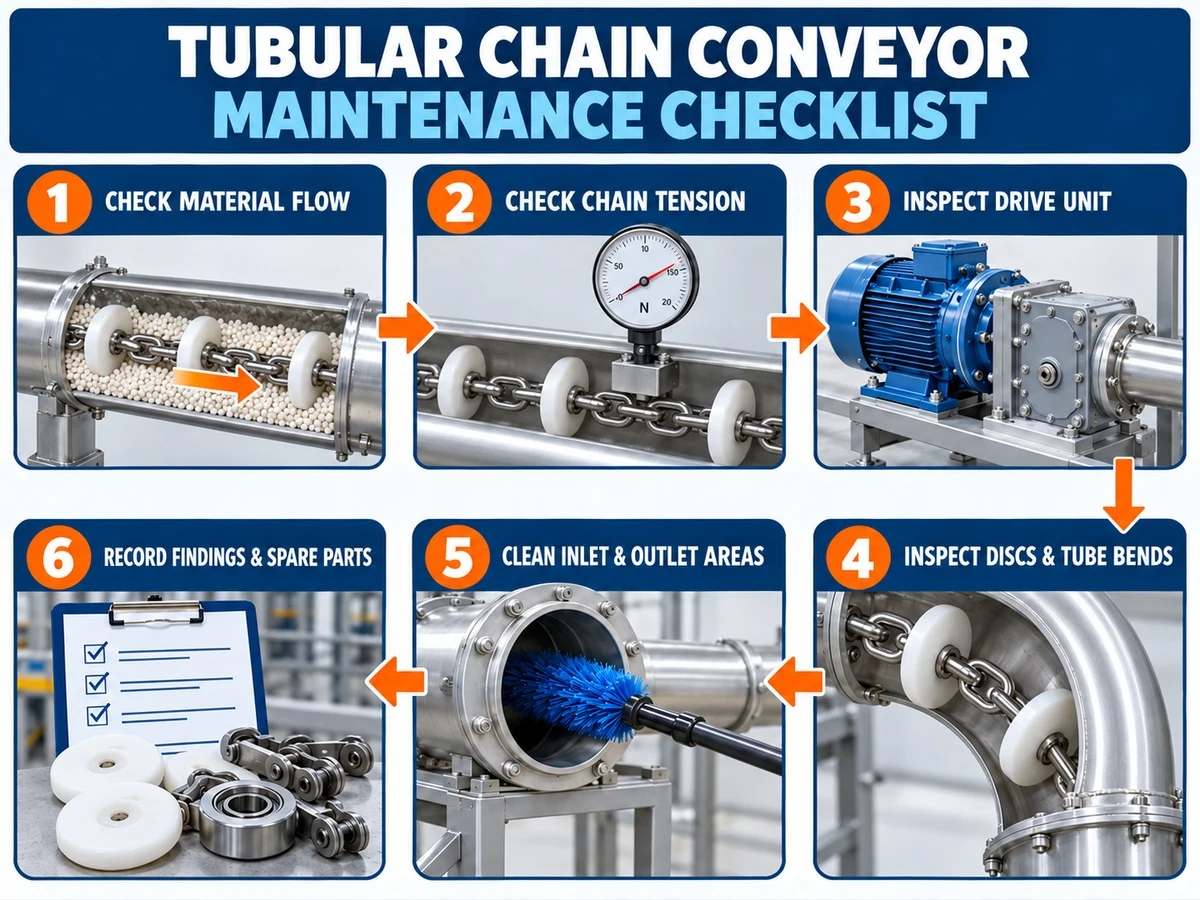
| Weekly | Check chain or cable tension, inspect accessible tube connections, clean inlet and outlet areas. | Do not wait until the chain becomes noisy or the motor overloads before adjusting tension. |
| Monthly | Inspect discs, bends, drive parts, bearings, seals, and fasteners. Confirm safety guards are secure. | Pay more attention when conveying abrasive powders, sticky powders, or high-density granules. |
| Quarterly | Review wear trend, lubrication records, spare parts inventory, and cleaning results. | Use this review to decide whether replacement should be planned before peak production. |
| Annual shutdown | Open inspection points, inspect the full route, replace worn parts, check alignment, and test the system after service. | Annual maintenance should be planned with production, maintenance, and safety teams together. |
Chain Tension and Movement: The First Maintenance Priority
Incorrect chain tension is one of the most common sources of tubular chain conveyor problems. Too much tension can increase wear and load on the drive system. Too little tension can cause unstable movement, poor material transfer, shock loading, or chain jumping in certain sections.
Operators should check tension according to the equipment manual and the actual running condition. If the conveyor has recently been installed, tension should be inspected more frequently during the early running period because chain or cable seating and material load conditions may change after commissioning.
Signs that chain or cable tension needs attention:
- New knocking or clicking noise during operation
- Unstable material discharge or reduced capacity
- Drive motor current higher than normal
- Visible vibration around the drive or tension section
- Frequent start-up difficulty after loaded stops
How Material Properties Change the Maintenance Plan
Maintenance frequency should not be copied from one factory to another without considering material behavior. A conveyor moving dry plastic pellets may have a very different wear pattern compared with one moving abrasive mineral powder, sticky food powder, or oily granular material.
| Material Condition | Maintenance Risk | Recommended Focus |
|---|---|---|
| Abrasive powder | Faster wear on discs, bends, and tube surfaces | Increase wear inspection frequency and keep spare discs or tube sections available. |
| Sticky or moist powder | Build-up at inlets, outlets, bends, and inspection points | Improve cleaning routine and check for material accumulation before blockage occurs. |
| Fragile granules or pellets | Material breakage if speed, feeding, or route is not suitable | Monitor discharge quality and avoid excessive speed or rough handling. |
| Food or pharmaceutical material | Hygiene risk, cross-contamination, cleaning validation concerns | Use defined cleaning procedures, sanitation checks, and documented maintenance records. |
| High-temperature material | Seal aging, bearing stress, thermal expansion issues | Check seal materials, bearing temperature, and system suitability for temperature range. |
Cleaning Best Practices for Enclosed Conveying Systems
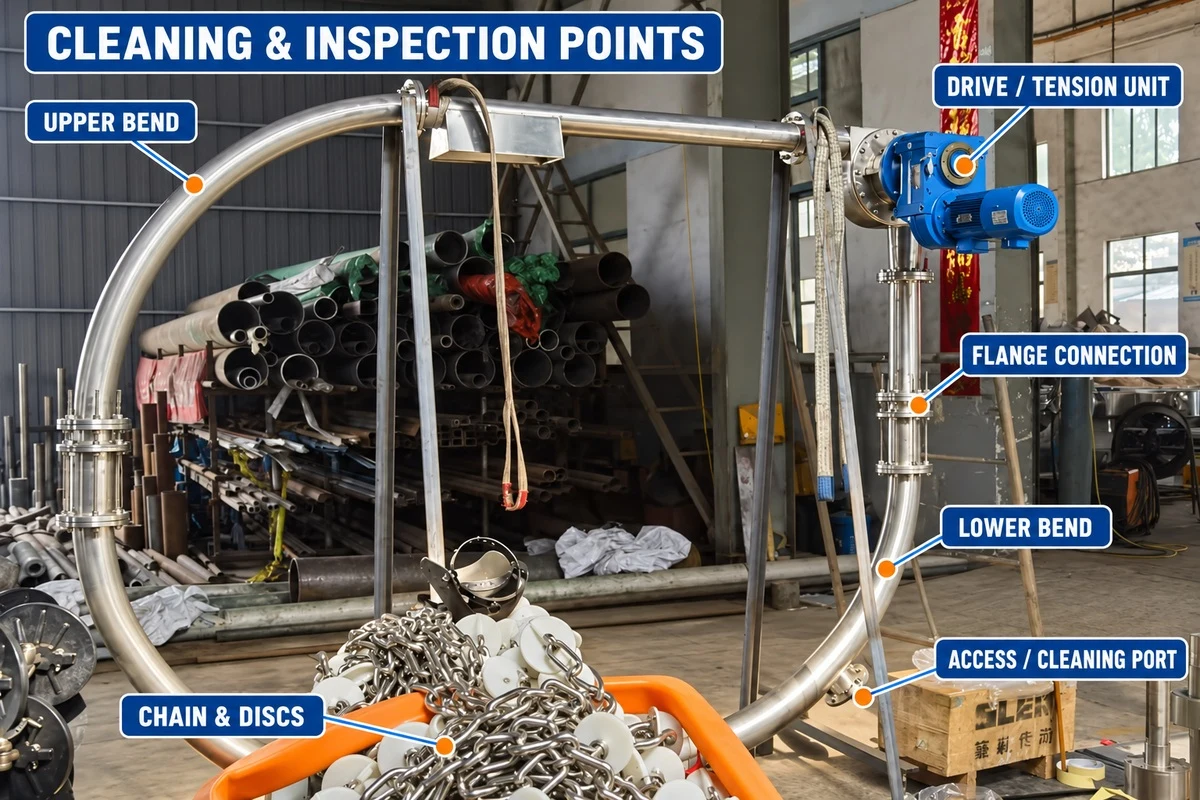
Cleaning is a maintenance task and a product-quality task at the same time. For food, chemical, pharmaceutical, and high-purity materials, cleaning helps prevent product contamination, color mixing, odor carryover, and material build-up inside the conveying route.
The right cleaning method depends on the material and system design. Dry cleaning may be enough for some powders and pellets. Other applications may require removable access points, air purging, brushing, flushing, or a validated sanitation process. The key point is that cleaning should be planned during conveyor selection, not added as an afterthought.
Spare Parts That Should Be Prepared in Advance
A good spare parts plan reduces downtime when a problem appears. For a tubular chain conveyor, the most important spare parts are usually the parts with predictable wear or parts that can stop the line if they fail.
- Chain or cable assembly, depending on conveyor design
- Conveying discs or flights
- Bearings, seals, and gaskets
- Drive-related components such as coupling parts or gearbox consumables
- Inspection covers, clamps, and connection hardware
- Inlet or outlet wear parts, especially for abrasive materials
For plants that operate continuously, spare parts should be linked to production risk. A part that is inexpensive but causes long downtime should be kept in stock. UNITFINE can help customers review material properties, operating hours, and maintenance history to recommend a practical spare parts list.
Troubleshooting Common Tubular Chain Conveyor Problems
| Problem | Possible Cause | What to Check First |
|---|---|---|
| Reduced conveying capacity | Inlet restriction, material build-up, worn discs, incorrect feeding | Check feed consistency, outlet discharge, disc condition, and tube accumulation. |
| Abnormal noise | Chain tension issue, worn bearing, foreign material, misalignment | Stop safely, inspect tension, drive area, bends, and accessible tube sections. |
| Motor overload | Blocked route, overfeeding, high material density, too much friction | Check material load, tube blockage, chain movement, and drive condition. |
| Dust leakage | Loose connection, seal wear, poor inlet/outlet transition | Inspect clamps, gaskets, inspection covers, and discharge connection points. |
| Product contamination risk | Poor cleaning, old residue, damaged seals, incorrect changeover process | Review cleaning record, inspection ports, material contact surfaces, and gasket condition. |
Maintenance Records: What Should Be Documented?
Maintenance records help operators see patterns before failures happen. A simple log can include date, running hours, material handled, inspection findings, lubrication, tension adjustment, parts replaced, cleaning completed, and abnormal observations. For plants with strict hygiene or quality requirements, maintenance records also support internal audits and customer quality reviews.
When to Ask the Conveyor Manufacturer for Support
Some maintenance issues can be handled by trained plant staff. However, repeated problems may indicate that the conveyor selection, layout, feeding method, or material behavior needs review. Contact the manufacturer when the same problem appears again after adjustment, when parts wear faster than expected, or when the material has changed since the conveyor was originally selected.
If you are comparing conveyor types, UNITFINE can also help review whether a conveying system, U type screw conveyor, vacuum conveyor, bucket elevator, or tubular chain conveyor is more suitable for your material and layout.
Need Help Maintaining or Upgrading a Tubular Chain Conveyor?
Share your material name, bulk density, moisture condition, conveying distance, lift height, operating hours, current maintenance issue, and photos of the conveyor route. UNITFINE can help review wear points, cleaning needs, spare parts, and possible upgrade options for a more reliable conveying line.
FAQ
How often should a tubular chain conveyor be inspected?
Basic visual checks should be done daily or each shift. Chain tension, inlet/outlet cleanliness, visible leakage, and abnormal noise should be checked regularly. A deeper inspection of discs, bends, bearings, seals, and drive components can be scheduled monthly or quarterly depending on running hours and material abrasiveness.
What is the most common maintenance issue in tubular chain conveyors?
Common issues include incorrect chain tension, material build-up at inlets or outlets, worn discs, bearing noise, and tube wear at bends. The exact issue depends on material properties and the conveyor route.
Can one maintenance schedule fit all materials?
No. Abrasive powders, sticky materials, fragile granules, food ingredients, and chemical powders require different inspection and cleaning frequencies. The maintenance plan should be adjusted to material behavior and production risk.
Should cleaning be considered during conveyor selection?
Yes. Cleaning access, inspection points, removable parts, and changeover requirements should be considered before the conveyor is built. This is especially important for food, pharmaceutical, chemical, and high-purity applications.
When should worn conveyor discs be replaced?
Discs should be replaced when wear affects material movement, when cracking or deformation appears, or when the conveyor begins to lose capacity because the discs no longer push material effectively. The replacement timing should be based on inspection records and operating conditions.
Can UNITFINE help with spare parts planning?
Yes. UNITFINE can review the conveyor model, operating hours, conveyed material, maintenance history, and production risk to recommend a practical spare parts list for chain or cable assemblies, discs, seals, bearings, and other wear components.